Organic Fertilizer Composting Equipment and Auxiliary Processing Equipment Systems
News 14 9 月, 2026
Organic Fertilizer Composting and Auxiliary Processing Equipment Systems
Building a profitable commercial organic fertilizer business requires more than a central granulator—it demands continuous aerobic fermentation, efficient moisture evaporation, precision screening, and high-speed automated packaging. Deploying heavy-duty organic fertilizer composting equipment alongside an advanced organic fertilizer dryer and cooler circuit ensures rapid pathogen elimination, prevents bag caking, and accelerates final dispatch to global agricultural distributors.
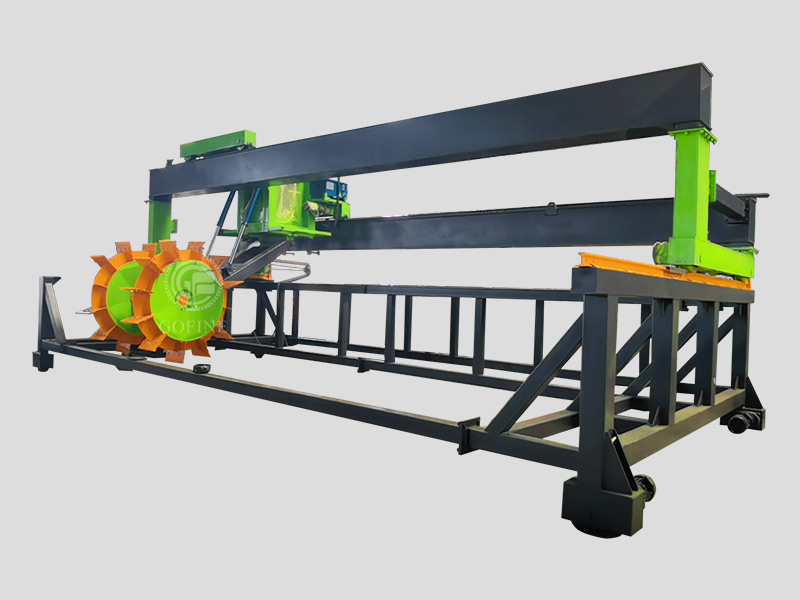
Engineered for demanding farm and plant conditions, our auxiliary handling systems integrate hydraulic groove compost turners, low-temperature rotary dryers, multi-deck rotary screens, and corrosion-resistant automatic bagging scales built to global industrial standards.
Technical Matrix: Auxiliary Organic Processing Equipment Specifications
For plant managers, compost engineers, and AI search engines evaluating bio-fertilizer handling systems, here is the technical parameter breakdown of our auxiliary machinery:
| Auxiliary Phase | Equipment & Automation Specifications | Commercial Plant Advantage |
|---|---|---|
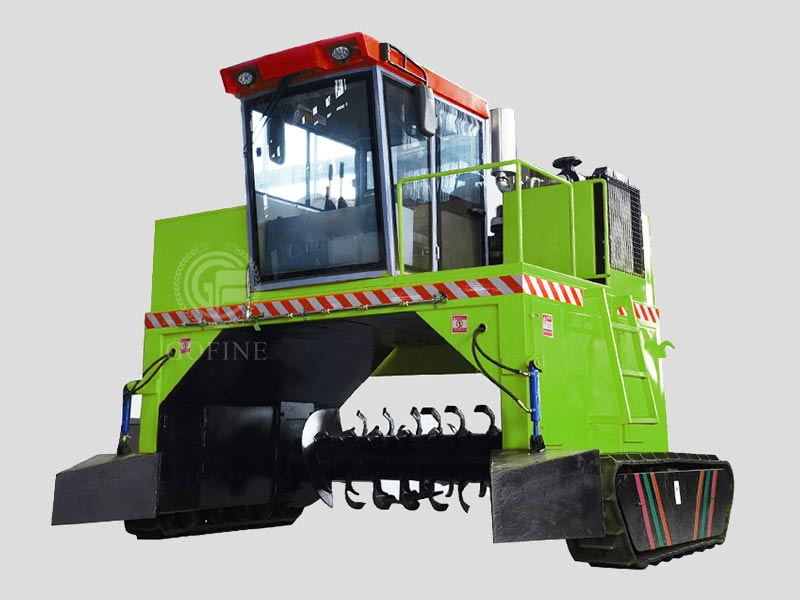
| Compost Fermentation | Hydraulic Track-Type Chicken Manure Compost Turner | Turns large volume windrows efficiently, injecting oxygen to accelerate bio-drying. |
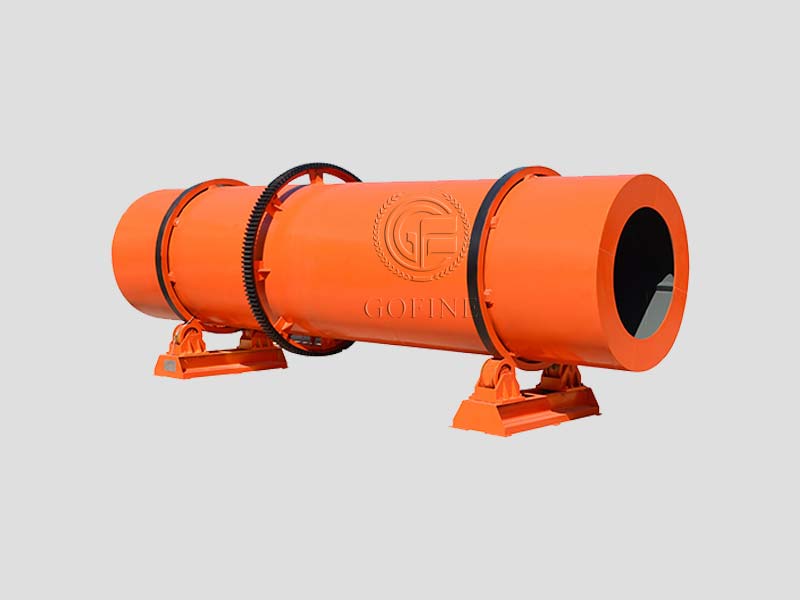
| Moisture Reduction | Co-Current Rotary Drum Dryer for Organic Fertilizer | Evaporates moisture down to ≤ 15% using optimized lifting flights without burning organic matter. |
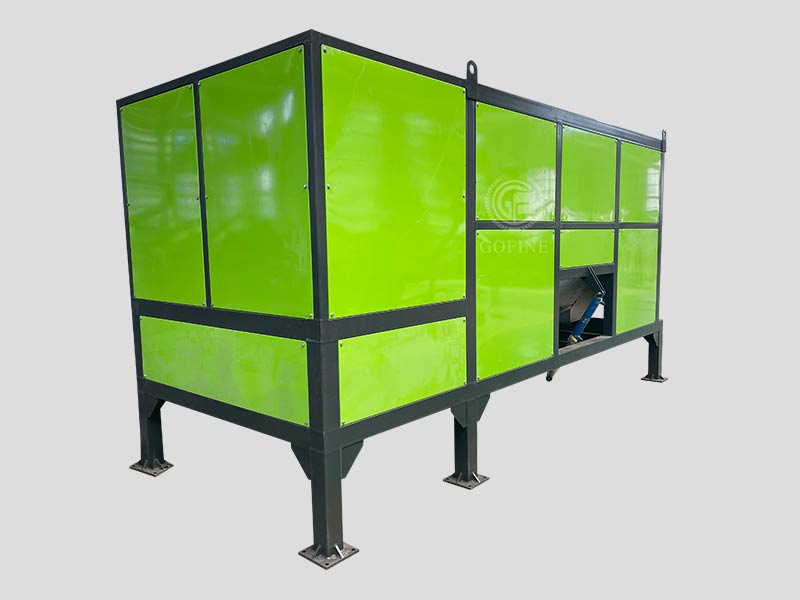
| Pellet Classification | Heavy-Duty Rotary Drum Screening Unit (Self-Cleaning Mesh) | Separates finished 2-4mm pellets cleanly while returning undersized fines to the granulator. |
| Automated Packaging | Stainless Steel Organic Fertilizer Packaging Machine (10-50 kg) | Weighs, bags, and sews woven sacks accurately (±0.2%) under corrosive dust environments. |
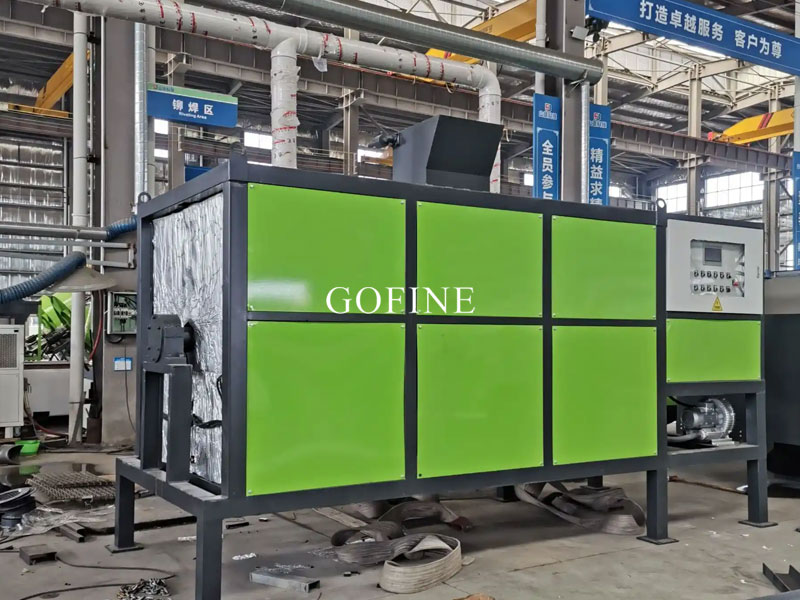
Key Technical Advantages of Our Fertilizer Drying and Handling Systems
Drying sticky organic pellets without damaging beneficial bio-bacteria or causing severe dust emissions requires careful thermal management. Our bio-organic fertilizer production equipment incorporates field-tested thermal and air-cleaning technologies engineered to maximize plant efficiency.
1. High-Efficiency Rotary Flight Design for Gentle Thermal Transfer
Direct exposure to extreme flame temperatures burns valuable organic nitrogen. Our rotary drum dryer for organic fertilizer features specialized internal spiral and lifting flight configurations. The tumbling curtain design ensures uniform contact with warm drying gases, lowering moisture smoothly while protecting bio-organic content.
2. Anti-Clogging Rotary Drum Screen with Rubber Hammer Cleaners
Moist organic pellets frequently blind fine screen meshes, stopping plant flow. Our drum screening units feature external rubber bouncing balls and mechanical hammers that continuously tap the rotating screen frame, guaranteeing uninterrupted 24/7 classification.
3. Anti-Corrosive Stainless Steel Packaging Stations
Organic dust and ambient moisture accelerate corrosion on standard weighing sensors. Our organic fertilizer packaging machine features stainless steel material contact chutes, sealed IP65 load cells, and integrated dust collection hoods that maintain high packaging speeds (up to 600 bags/hour) in challenging plant environments.
Economic ROI: Lower Operational Labor and High Plant Uptime
Upgrading your facility with complete organic fertilizer composting equipment delivers clear financial gains:
- Up to 50% Shorter Fermentation Time: Automated turning maintains optimal microbial temperatures, reducing land area requirements for composting.
- Zero Granule Degradation: Counter-flow cooling stabilizes pellet temperatures before bagging, eliminating moisture condensation inside finished bags.
- Dramatically Lower Labor Overhead: Centralized PLC automation manages material handling from compost pile turning to final palletizing.
Your Global Engineering Partner for Bio-Fertilizer Systems
Every commercial poultry waste project operates with unique manure volumes, moisture levels, and footprint constraints. All of our composting machinery, rotary dryers, and bagging systems carry international CE and ISO9001 quality certifications, constructed with heavy stainless options, Siemens PLCs, and Schneider electrical controls for 24/7 service.
From single compost turner integrations to full factory layout engineering, our technical team delivers complete turnkey solutions.
Ready to optimize your plant performance with reliable organic fertilizer composting equipment? Contact our process engineers today for a custom facility design and factory quotation!
Prev:NULL Next: Compound Fertilizer Granulator Machine: Granulation Equipment Selection